 GET QUOTE
 NEWSLETTER
 LOGIN


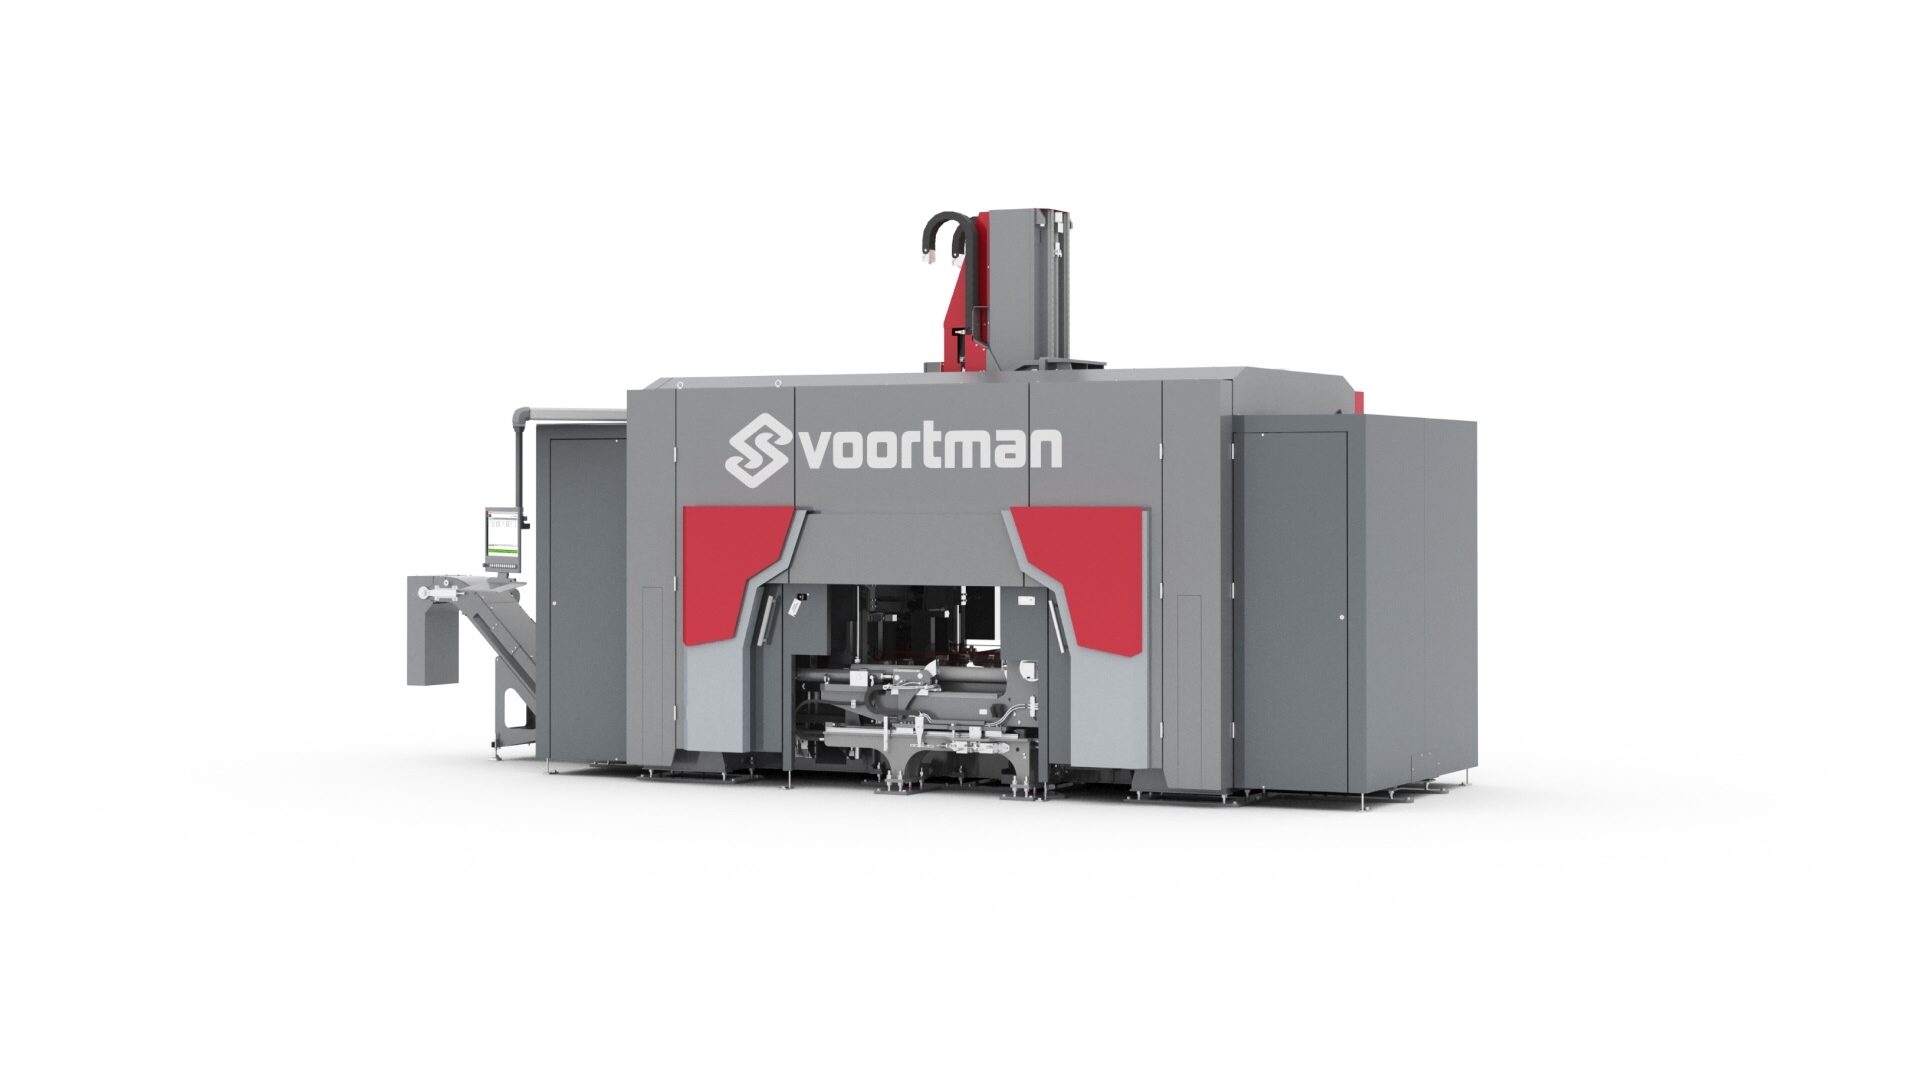
DEMO - V633: Offset drilling with sub-axes
Watch the video or continue reading to learn how the V633 drills holes at different X-positions using its sub-axes.
The video shows how the V633 uses its sub-axes to independently position the drilling units along the length of the profile. This allows the V633 to drill holes at different positions without having to move the entire profile each time. Within the available sub-axis stroke, each spindle can move to the required position while the profile remains in place. In simpler terms, each drilling unit can move slightly forward or backward on its own to reach the next hole or feature.
This is especially useful when a part has many holes, threaded holes, markings or milled features that do not line up at the same position. Instead of moving the whole profile back and forth for every operation, the drilling units can move to where they are needed. This also creates more opportunities to process features at different positions on multiple sides at the same time. The result is less unnecessary movement and faster processing, especially for complex parts with many features.
These small, independent movements of the drilling units are what we call the sub-axes. Put simply: the profile does not always have to move to the tool; the tool can also move to the right position on the profile.

REFERENCES & RESOURCES