 GET QUOTE
 NEWSLETTER
 LOGIN


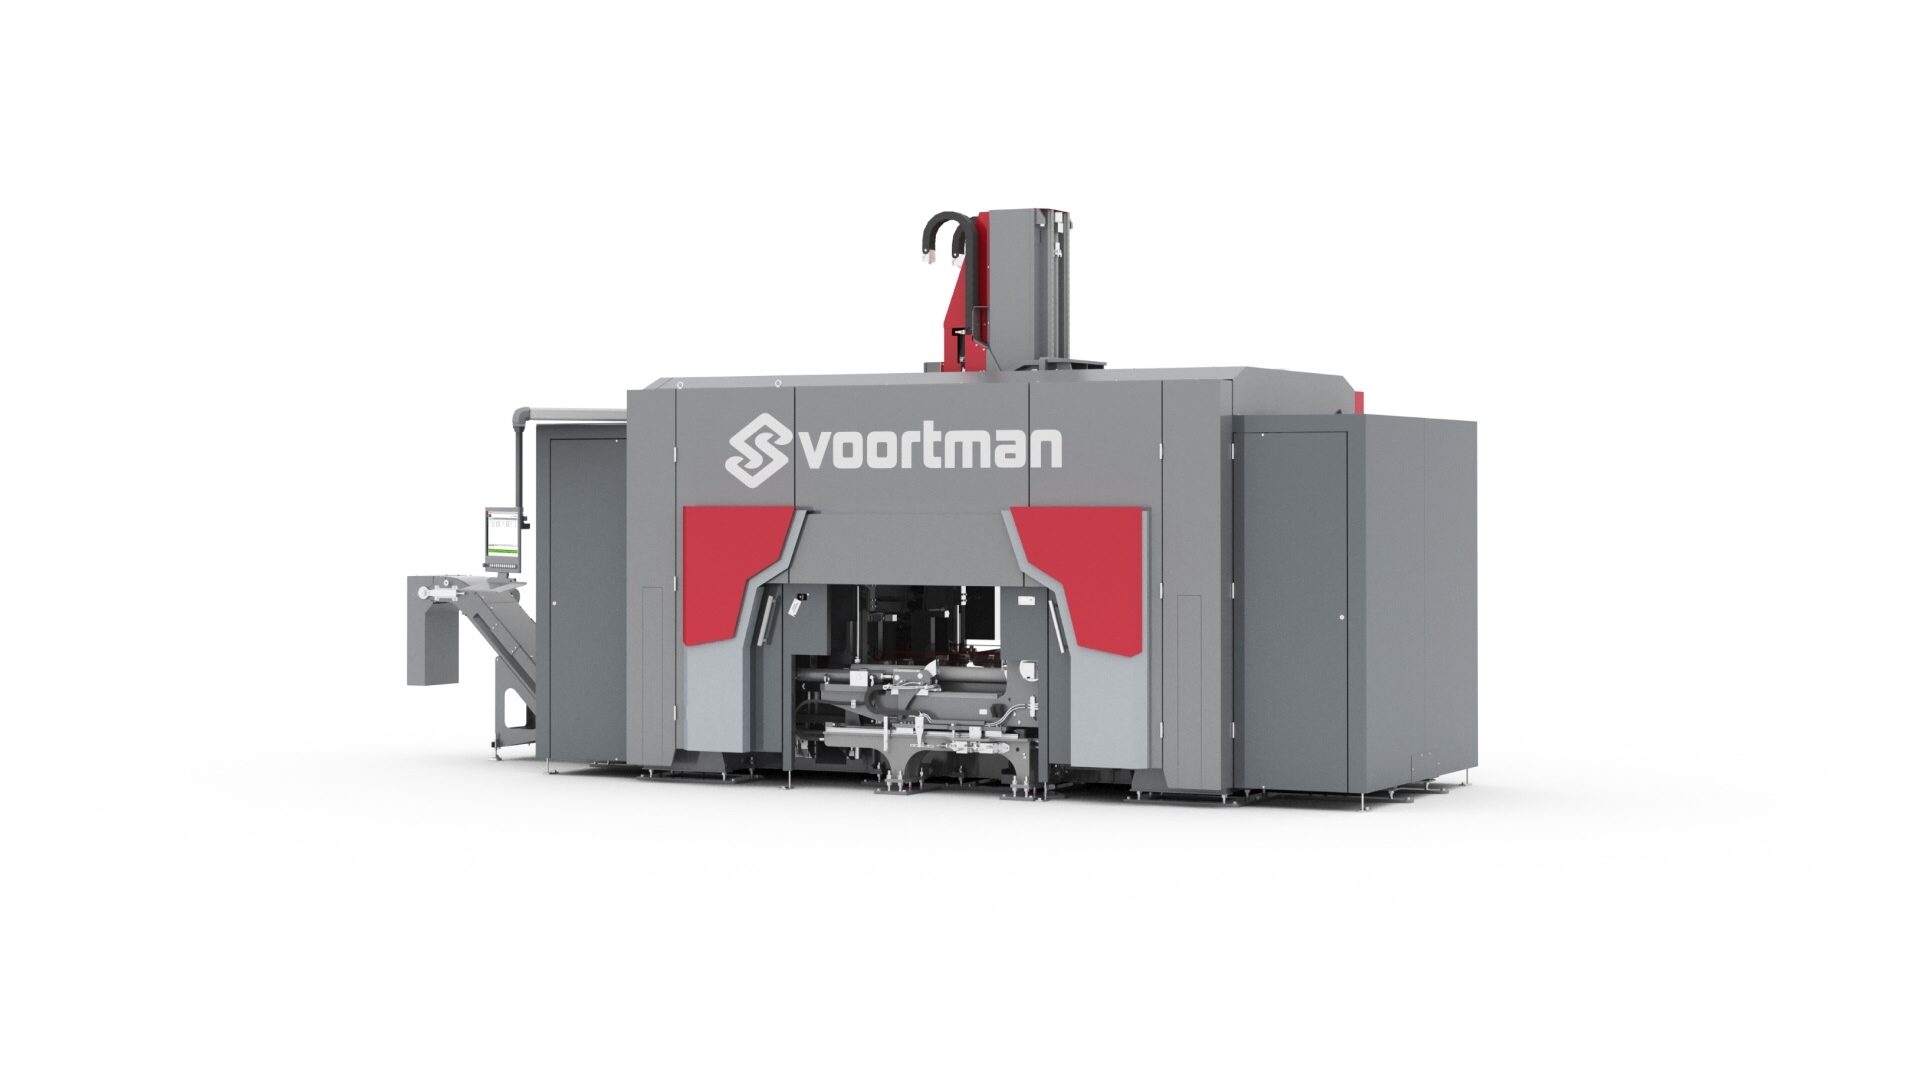
DEMO - V633: Simultaneous milling with sub-axes
Watch the video or continue reading to learn how the V633 uses its sub-axes to mill slotted holes on two sides of a profile at the same time.
Slotted holes are elongated holes that provide more room for positioning and adjustment than standard round holes. When slots are required on different sides of a steel profile, these features need to be processed accurately at their specified positions.
This demo shows the V633 milling slotted holes on two sides of the profile simultaneously. Instead of completing the milling operation on one side before moving on to the other, two processing units can work at the same time.
The V633's servo-driven sub-axes make this simultaneous processing possible. They allow the processing units to independently adjust their position along the length of the profile within a 300 mm (11 13/16") range. In simple terms, the processing units can move to where they are needed without always having to reposition the entire steel profile.
This independent movement is especially valuable when multiple features need to be processed at different positions or on different sides. Rather than treating every operation as a separate step, the V633 can perform operations simultaneously when their positions fall within the available sub-axis range.
For the customer, the principle is simple: if two slotted holes can be milled at the same time instead of one after the other, less time is needed to process the profile. Combined with reduced profile movement, the sub-axes help make complex milling work more efficient.

REFERENCES & RESOURCES